Plasma POST Processor Requirements
Requirements for a post processor for MASSO Version 5 software with the MASSO DTHC, for users who want to write their own. Because many plasma functions are built into MASSO, the G-code is much simpler than older plasma posts.
Software
MASSO V5 and later
Height control
THC or DTHC
Tool
T112 (Plasma)
CAUTION
Posts written to these requirements do not work with Version 4 plasma software or earlier.1. What the post must output
2. Automating S0 / S1
The G200 S value can be set by the post in two ways:
3. Sample G-code file
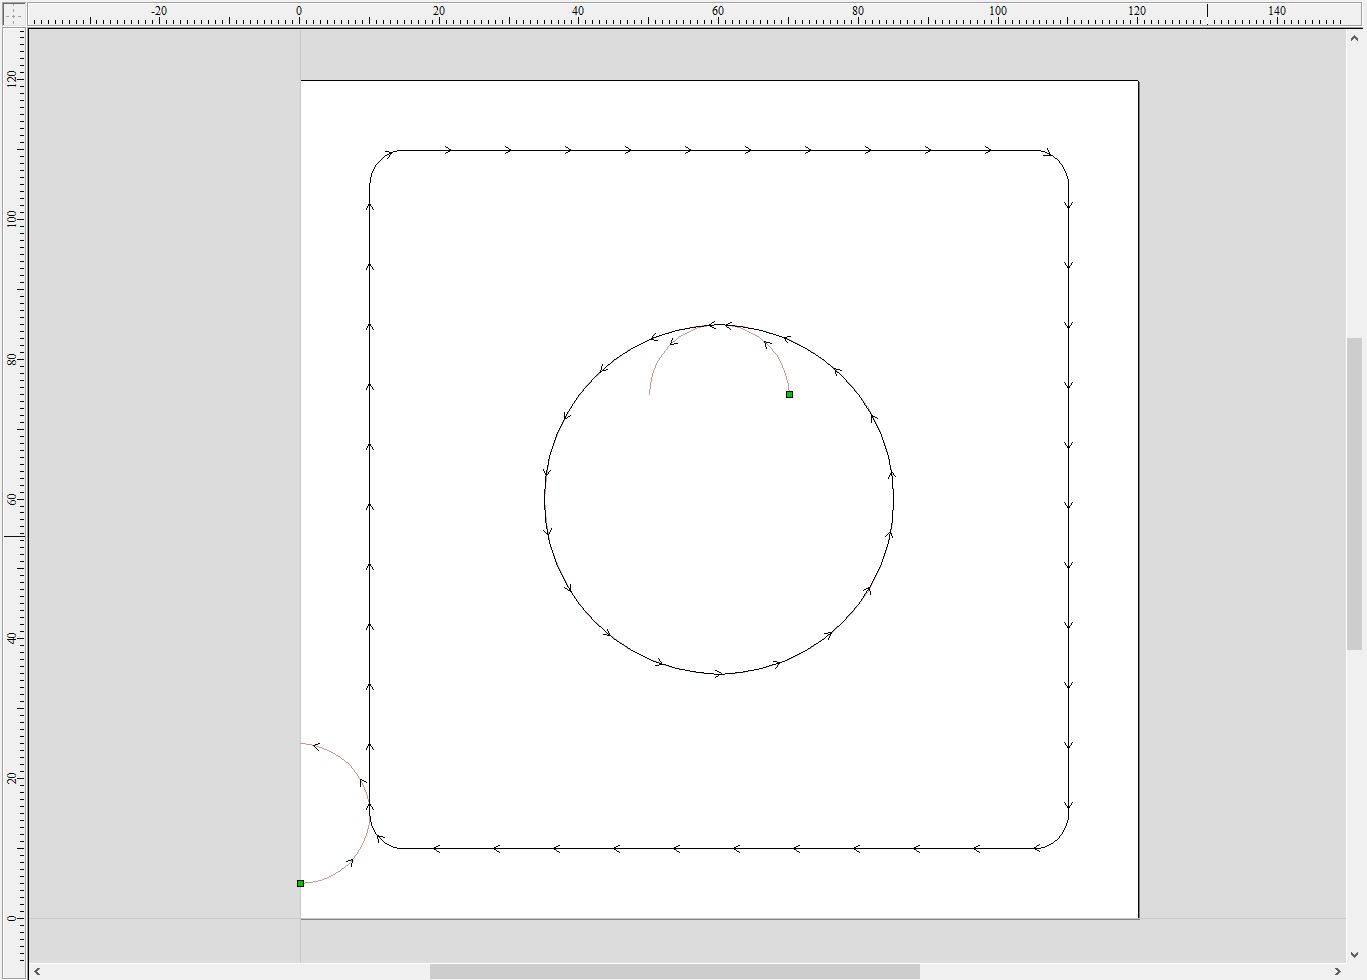
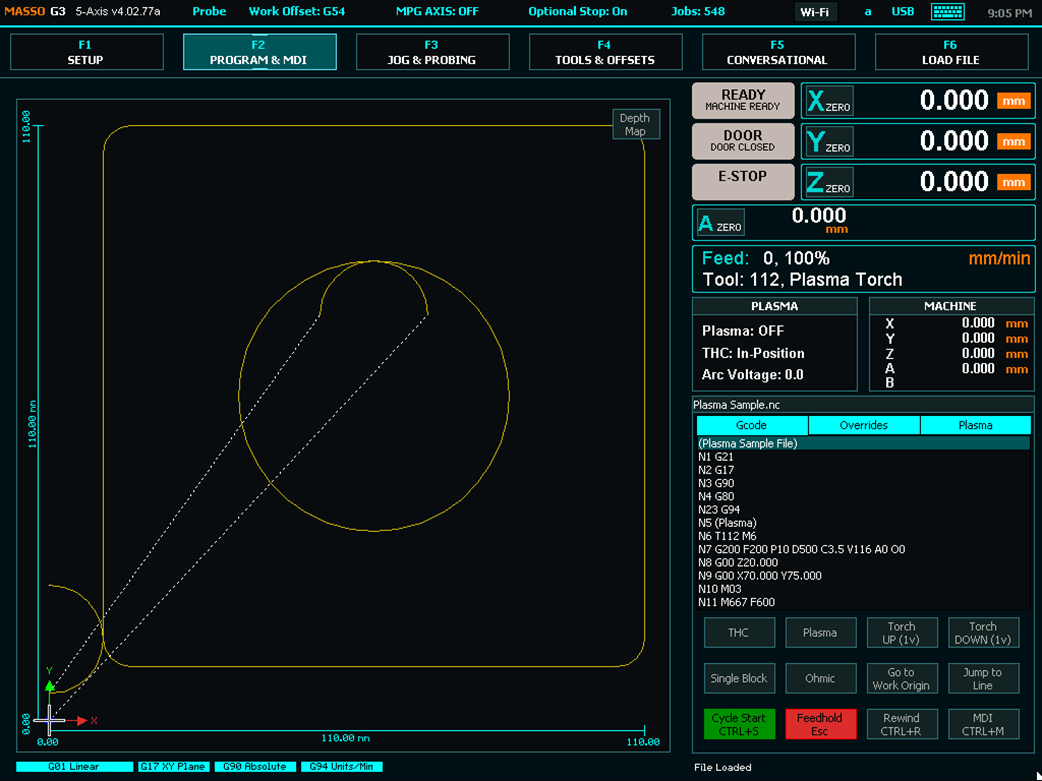
A sample file with G200, M667 and M666. Comments are in brackets.
(Plasma Sample File)
N1 G21
N2 G17
N3 G90
N4 G80
N23 G94
N5 (Plasma)
N6 T112 M6  (This is required to put MASSO into Plasma Mode. The Tool number must always be Tool 112)
N7 G200 F200 P10 D500 C3.5 V116 A0 O0 S0 (This Gcode sets the Plasma Parameters)
N8 G00 Z20.000 (Safe Z move)
N9 G00 X70.000 Y75.000
N10 M03 (Turn Plasma on, Probe, Delay, Set cutting height)
N11 M667 F600  (This will Turn the THC on at a Z axis feed rate of 600mm/min)
N12 G03 X60.000 Y85.000 I-10.000 J0.000 F3000
N13 G03 X35.000 Y60.000 I0.000 J-25.000
N14 G03 X60.000 Y35.000 I25.000 J0.000
N15 G03 X85.000 Y60.000 I0.000 J25.000
N16 G03 X60.000 Y85.000 I-25.000 J0.000
N17 G03 X50.000 Y75.000 I0.000 J-10.000
N18 M666 (This Turns the THC off)
N19 M05 (Turns Plasma Off)
N20 G00 Z20.000 (Safe Z move)
N21 G00 X0.000 Y5.000
N22 M03
N23 M667 F600
N24 G03 X10.000 Y15.000 I0.000 J10.000 F3000
N25 G01 X10.000 Y105.000
N26 G02 X15.000 Y110.000 I5.000 J0.000
N27 G01 X105.000 Y110.000
N28 G02 X110.000 Y105.000 I0.000 J-5.000
N29 G01 X110.000 Y15.000
N30 G02 X105.000 Y10.000 I-5.000 J0.000
N31 G01 X15.000 Y10.000
N32 G02 X10.000 Y15.000 I0.000 J5.000
N33 G03 X0.000 Y25.000 I-10.000 J0.000
N34 M666
N35 M05
N36 G00 Z20.000 (Safe Z move)
N37 M30
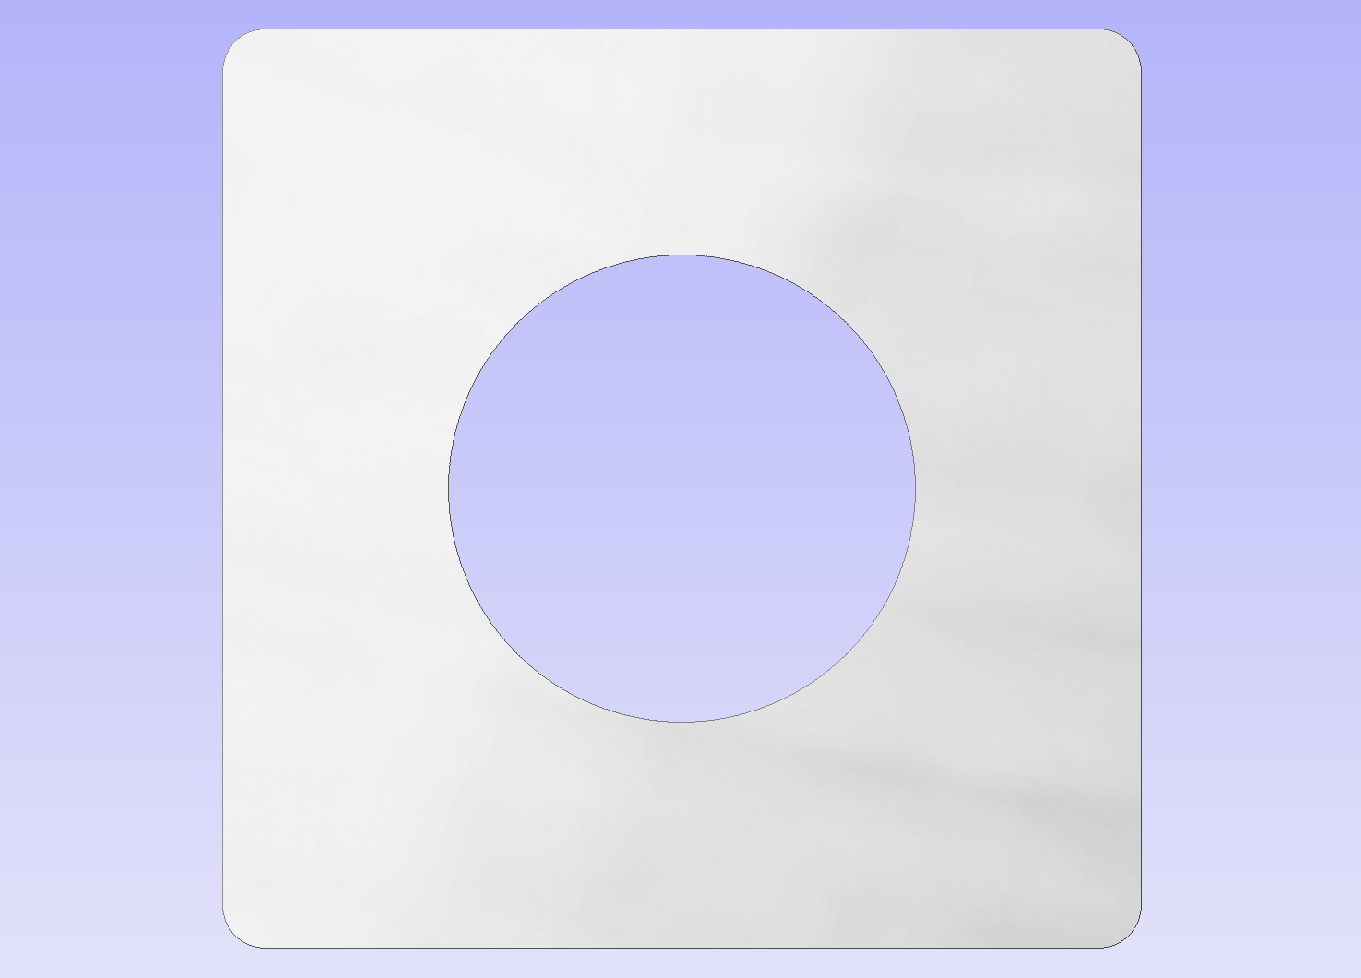
4. Sample results