G38.6 - Digitizing Probing Cycle
G38.6 digitises parts with a touch probe or similar device. Use it to capture a point cloud of a 3D object, or to map an uneven material surface for engraving with auto-levelling software.
Syntax
G38.6 Z-3 F100
Coordinates
Working coordinates
Not available on
MASSO G2
WARNING
Incorrect use of G38.6 can damage the probe and the item being probed, and can cause injury. Make sure you fully understand the probing process and take extreme care with this command.1. How it works
All coordinates used by G38.6, and all values written to the file, are working coordinates. A probe input must be assigned, and it must change from Low to High when the probe triggers.
2. Parameters
3. Example
N10 G1 X20 Y10 F1000
N20 G38.6 Z-3 F100
N30 G0 Z2
If the probe doesn't trigger before Z−3, the machine stops, a Probing Error alarm is shown, and this line is written to the file:
Probing error at: 20.00000, 10.00000
4. Sample data file
0.00000, 0.00000, -0.88750
0.13310, 0.00000, -0.90749
0.26619, 0.00000, -0.91750
0.38597, 0.00000, -0.92249
Probing error at: 0.00000, -0.92000
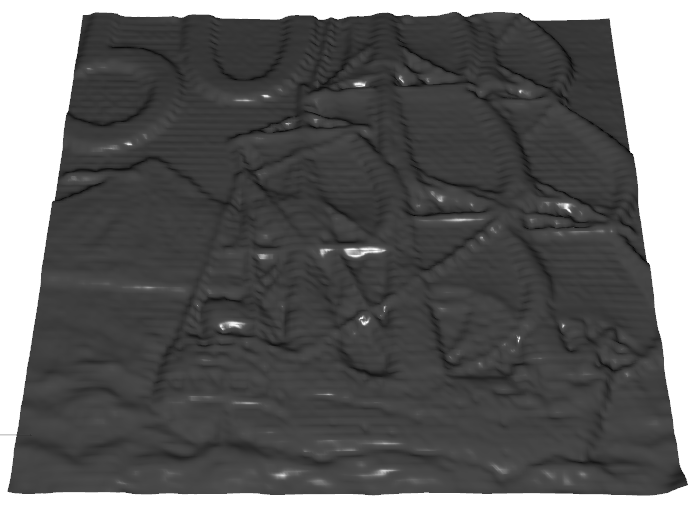
5. Sample digitised item