M667 – Plasma – Turn THC Function On
On MASSO plasma, M667 turns on THC (torch height control) automatic Z-axis control. F sets how fast Z moves the torch up and down under THC. It takes effect on the next axis move.
Syntax
M667 F__
Machine
Plasma
Takes effect
Next axis move
1. Parameters
2. Examples
N10 M667 F500
N20 G01 X1 F1000
Turns THC on with a THC feed rate of 500, from the next axis move.
N10 M667
N20 G1 X1 F1000
Turns THC on using the last M667 feed rate (or the axis maximum if none has been set), from the next axis move.
3. Choosing the THC feed rate
Adjusting it while cutting
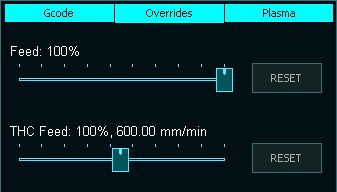
Use the THC feed rate slider on the Overrides page to adjust it in real time. The slider shows the current value, which you can use as a starting point for future cuts in the same material.
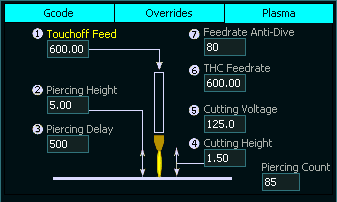
You can also see the current THC feed rate on the Plasma page and type a new value in the box. It stays active until replaced by a new entry or a G-code command.