How MASSO Plasma Works
How a plasma cut runs on MASSO: selecting the plasma tool, what G200 and M3 do, and the F2 Plasma and Overrides tabs you use while cutting.
Selecting the plasma tool
Plasma only works with Tool 112 selected. Select it with T112 M6 in the G-code (ideally in the file header) or in MDI. MASSO stays on Tool 112, including through power off and on, until another tool is selected. Selecting any other tool cancels plasma mode.
The plasma cycle
G200 sets the cutting parameters and automates touch-off, piercing and moving to cut height. It's required for the MASSO DTHC and recommended for legacy THC units. MASSO handles all Z moves while cutting, so your G-code only needs to move to a safe Z between cuts.
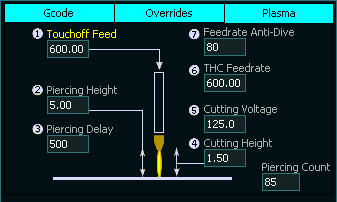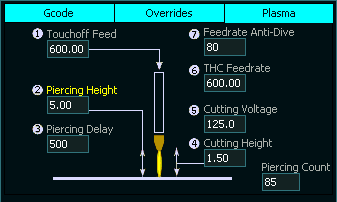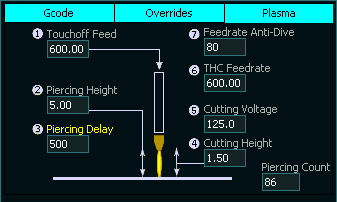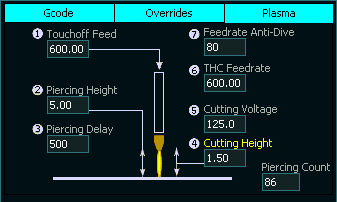
T112 M6 selects the plasma tool. On a multi-head machine the Plasma Up/Down output goes high to move the torch into position.G200 values fill in the Plasma tab.M3 starts the cycle: the torch touches off on the material, moves to pierce height and fires the arc.M667 F… turns THC on. The DTHC moves Z to hold the cutting voltage; F sets the Z speed under THC.M666 turns THC off and M5 turns the arc off.With a legacy THC unit the cycle is the same, but the voltage is set on the THC unit and the G200 V value is ignored.
F2 Plasma tab
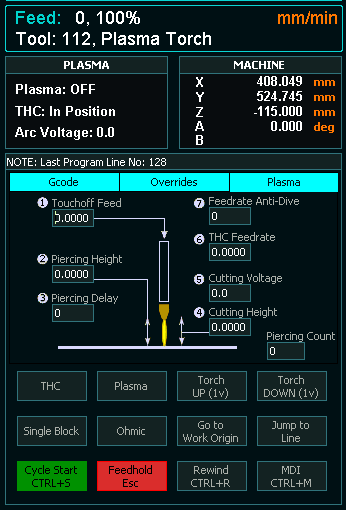
Click a box to type a new value. You can do this while cutting to fine-tune the cut. Torch Up and Torch Down change the cutting voltage by 1 V per press.
 Arc time
 Pierce count
Overrides tab
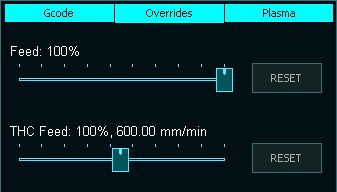
If Z oscillates while the DTHC is holding height, lower THC Feed until Z moves smoothly and follows the material. Note the value and use it as the M667 F value in future files. Reset returns both sliders to 100%.