This tool changer is for MASSO G3 and MASSO G3 Touch only and is available in Beta v5.100b.
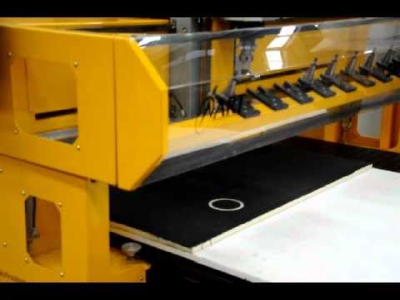
In a traveling linear tool changer, the tools are mounted along the X axis and move with the X-axis gantry. The tool tray takes part in the tool change, positioning tools for loading and unloading.
Slots
4 to 30
Slot position
X only
I/O
3 inputs, Chuck Clamp + 3 outputs
1. Select the tool changer
In the Tool Changer window, select Linear Tool Changer and double-click it to open the settings.
sets how long (ms) the air blast cleans the tool setter after a tool change, before measuring. Assign its output as Tool Setter Air Blast.
2. Settings
CAUTION
For a traveling tool changer, Tool tray fixed to X-axis must be ticked and Load and unload tools without sliding must be unticked.
Parameter
Description
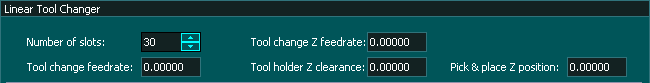
Number of Slots
4 to 30.
Tool Change Z Feedrate
Z speed during the tool change.
Tool Change Feedrate
X/Y speed for sliding tool changers – not used on traveling tool tray systems.
Tool Change Z Clearance
Safe Z height (machine coordinate) after dropping off a tool.
Pick and Place Z Position
Z height (machine coordinate) for placing or picking up a tool.
Tool slots
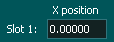
X Position sets the centre of each tool slot, as a machine coordinate.
3. Inputs and outputs
“Tool Changer - Input 1” and “Tool Changer - Output 1” are function names, not physical ports – assign them to any free MASSO input or output. Leave unused ones unassigned and MASSO ignores them.
Input
Signal
1
Drawbar: Low = clamped, High = unclamped
2
Tool in place: Low = no tool in spindle
3
Spindle INDEX position
Output
Controls
Chuck Clamp (M10/M11)
Clamp/unclamp spindle tool
1
Air return (High for 6 s after the change)
2
Spindle clean air blast
3
Spindle INDEX control
INFORMATION
To invert any input or output, select it and press Space. The change is saved automatically.
4. Tool change sequence
#
Action
1
Spindle off; MASSO waits for the Spin Down Delay.
2
Checks that the current and requested tools are each assigned to a slot.
3
Z moves to home; the tool tray moves up.
4
X and Y move to the unload start position; Z descends to the Pick and Place Z Position and slides into the holder.
5
Unclamp: Chuck Clamp High, wait up to 6 s for Input 1.
6
Z rises to the Tool Change Z Clearance; X and Y move to the new tool.
7
Output 2 (air blast) High while Z descends to the Pick and Place Z Position, then Low.
8
Clamp: Chuck Clamp Low, wait up to 6 s for Input 1.
9
Tool check: Input 2 must go High, otherwise a Tool Error alarm shows.
10
Z slides out of the holder; Output 1 (air return) High for 6 s; the tool tray moves down.

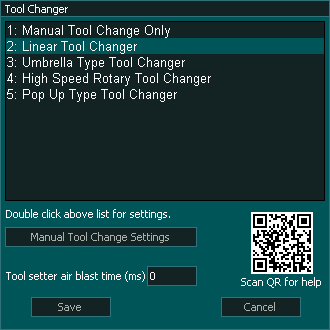
 sets how long (ms) the air blast cleans the tool setter after a tool change, before measuring. Assign its output as Tool Setter Air Blast
 .
 and Load and unload tools without sliding must be unticked
 .