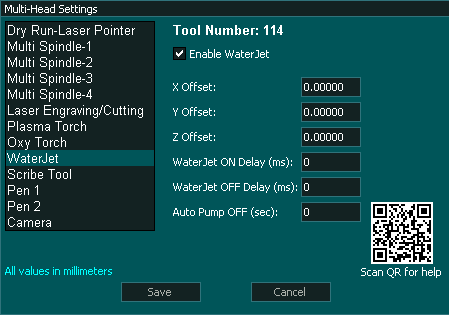
MASSO controls waterjet cutting heads as tool 114: pump, cutting valve, abrasive feed, low-pressure piercing and bleed-off, with alarms for cut sense, breakaway, pressure and abrasive.
Selecting the waterjet
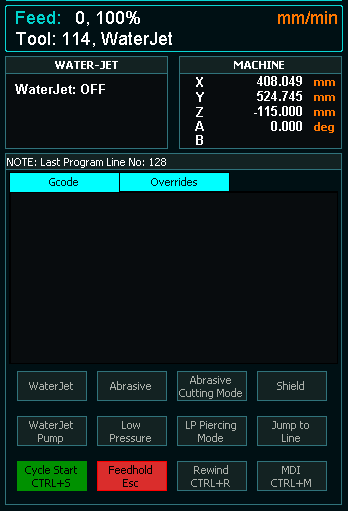
Run T114 M06 in MDI, and put it at the start of your G-code file so the right screen is active when the job runs. M03 starts the waterjet and M05 stops it. There are no other waterjet G-codes: the cutting mode is set with buttons on the F2 screen.
Cutting modes
Two buttons on the F2 screen set the mode: Abrasive and Low Pressure. A button is yellow when on.
| Mode | Buttons | Use |
|---|
| Water only |   | Water only, no abrasive |
| Abrasive |  | Water and abrasive |
| Abrasive with low-pressure piercing |  | Water and abrasive, pierce at low pressure, then cut at full pressure |
Output sequence for each mode
After Cycle Start, MASSO runs these steps on M03 and M05. Motion between them follows the G-code.
Water only
ON M03
- On/Off output high
- Wait for Cut Sense high
ON M05
- On/Off output low
Abrasive
ON M03
- Abrasive output high
- Wait ON Delay
- On/Off output high
- Wait for Cut Sense high
ON M05
- Abrasive output low
- On/Off output low
Abrasive + low-pressure pierce
ON M03
- Low Pressure output high
- Abrasive output high
- Wait ON Delay
- On/Off output high
- Wait for Cut Sense high
- Low Pressure output low (full pressure)
ON M05
- Abrasive output low
- Low Pressure output high (bleed-off)
- Wait OFF Delay
- On/Off output low
Each button shows its current state, turns yellow when on, and toggles on or off when pressed.
| Button | Function | Screen |
|---|
 | WaterJet on/off (cutting valve) | F2 |
 | Abrasive feed on/off | F2 |
 | Low pressure on/off | F2 |
 | Pump on/off | F2 |
 | Raise or lower the shield manually | F2 |
| Abrasive cutting mode | F2 |
| Low-pressure piercing mode | F2 |
 | Air on/off | MDI only |
 | Tap water on/off | MDI only |
| Input | What it does |
|---|
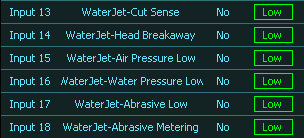
| WaterJet – Cut Sense | Feedback from the cutting valve, active high. If it doesn't go high within 12 seconds of the jet starting, or goes low while cutting, a Cut Sense alarm stops the machine. If your machine has no cut sense signal, leave this unassigned: cutting starts as soon as the ON Delay ends. |
| WaterJet – Head Breakaway | Goes high if the head hits material or comes loose. Stops the machine with an alarm. |
| WaterJet – Air Pressure Low | Alarm when high. |
| WaterJet – Water Pressure Low | Alarm when high. |
| WaterJet – Abrasive Low | Abrasive level. Alarm when high. |
| WaterJet – Abrasive Metering | Abrasive metering system fault. Alarm when high. |
Outputs
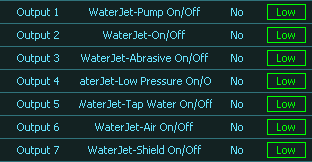
| Output | What it does | Controlled by |
|---|
| WaterJet – Pump On/Off | Main pump | Pump button (F2) |
| WaterJet – On/Off | Opens the cutting valve | M03 or WaterJet button (F2) |
| WaterJet – Abrasive On/Off | Abrasive feed; used in abrasive modes | Cutting sequence or Abrasive button (F2) |
| WaterJet – Low Pressure On/Off | Low-pressure piercing and high-pressure bleed-off | Cutting sequence or Low Pressure button (F2) |
| WaterJet – Tap Water On/Off | Tops up the water tank | Tap Water button (MDI, Ctrl+M) |
| WaterJet – Air On/Off | Air solenoid | Air button  (MDI, Ctrl+M) |
Timers and offsets
Set on the WaterJet page of Multi-Head Settings.
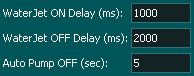
| Setting | What it does |
|---|
| WaterJet ON Delay (ms) | Time for low pressure and abrasive to set up before the cutting valve opens. |
| WaterJet OFF Delay (ms) | Time for high-pressure bleed-off at the end of a cut, before the jet turns off. |
| Auto Pump OFF (s) | Turns the pump off if no cut starts within this time. Restarts counting each time a cut ends. 0 = never turn off automatically. |
| X, Y, Z offsets | Waterjet head position relative to the reference head. Leave at 0 if the waterjet is the only head. |