G42 turns on cutter compensation to the right of the programmed tool path. The cutter is offset to the right-hand side by an amount calculated from the tool diameter, wear diameter and P value.
Syntax
G42 / G42 P5
Modal
Yes – Group 7
Applies to
MASSO G3 and G3 Touch (Advanced)
INFORMATION
Cutter compensation is part of the Advanced portfolio and works the same on both MASSO G3 and MASSO G3 Touch controllers. It's available for download through myWorkshop.
WARNING
Not following the cutter compensation rules (section 4) can cause unpredictable motion and damage the workpiece or the machine.
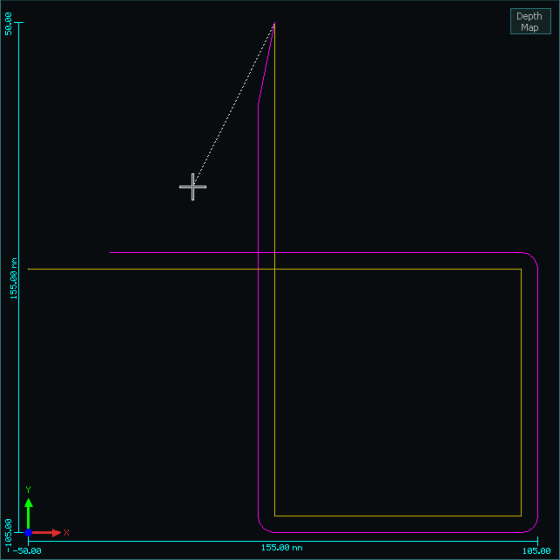
Compensation is turned on once the tool is at cutting depth, and a linear lead-in move is made before cutting starts. G40 then cancels compensation, and a lead-out move takes the tool to a safe location before it retracts. The lead-out isn't shown as a compensated move.
Compensated toolpath shown in purple.
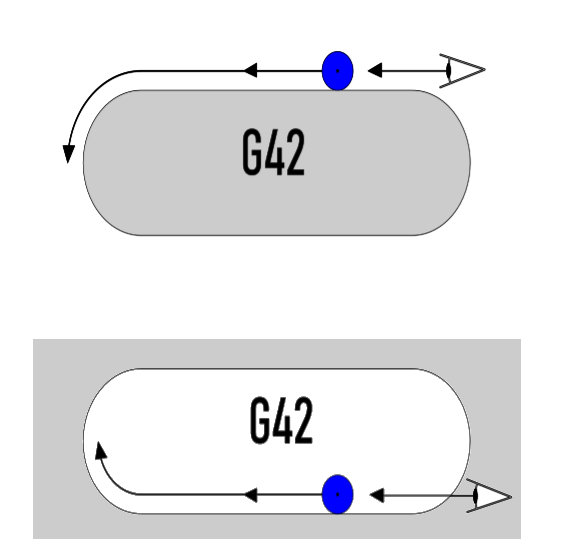
3. Understanding G42 direction
Imagine standing behind the cutter as it moves away from you. With G42 active, the cutter moves to the right-hand side of the programmed tool path.
4. Cutter compensation rules
Topic
Rule
Display
Compensated paths are calculated and shown when the G-code file is loaded. Outside corners are radiused automatically.
Plane and axes
Valid in the G17 XY plane only, for X and Y moves only. Don't include Z, A or B moves while compensation is active – results may be unpredictable.
Cutting depth
Move the tool to cutting depth before turning compensation on.
Other commands
Don't include non-cutting commands, such as coolant on or off, while compensation is active.
Lead-in / lead-out
A linear lead-in to a safe location is required before turning compensation on, and a linear lead-out to a safe location after cancelling it. Both must be linear moves only and longer than the cutter radius. The lead-out isn't shown as a compensated move.
Circles
Don't cut a complete circle with a single arc command.
After G40
Give both X and Y on the first move after cancelling compensation, to avoid unpredictable motion.
Jump to line
Don't use jump-to-line while compensation is active. To resume, rewind the program to a point before compensation was turned on.
5. Troubleshooting
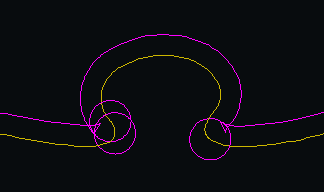
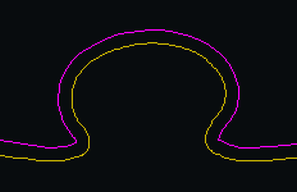
If the compensated path shows loops or self-intersections, the calculated cutter size is too large for the programmed geometry. Choose a smaller cutter that suits the job.
Cutter too largeCutter size correct
6. Managing Tool Diameter, Wear Diameter and P
MASSO cutter compensation works with both CAM-generated and hand-written G-code. The current tool's Tool Diameter and Wear Diameter are applied automatically whenever G42 is turned on, and the final offset always combines them with any P value in the G-code.
Value
How to use it
P value
Gives the cutter radius directly in G-code – e.g. P5 for a 10 mm cutter. Common in hand-written G-code, where you program the nominal geometry and let the controller apply the offset. Set the Tool Diameter to 0 so P controls the radius; any Wear Diameter is still included. P can be combined with a Tool Diameter if an application needs it, though this is uncommon.
Tool Diameter
Usually 0 when compensation is handled in CAM. When the G-code has no compensation (e.g. hand-written programs), use it to apply the offset. It can be the measured or the nominal diameter, with final sizing done by the Wear Diameter.
Wear Diameter
Fine-tunes the effective cutter size as the tool wears. Negative = undersized, positive = oversized. For a 10 mm cutter, −0.5 mm gives an effective 9.5 mm; +0.5 mm gives 10.5 mm.